Hey folks, if you’ve ever dived into the world of industrial sterilization—especially for medical devices, pharmaceutical packaging, or even delicate electronics—you’ve probably heard of EO sterilization. EO, short for ethylene oxide, is the workhorse of low-temperature sterilization because it kills even the tiniest pathogens without melting or damaging heat-sensitive gear. But here’s the thing that stumps a lot of folks when they’re first setting up or troubleshooting their EO process: the gas mixture ratio. I’ve been selling industrial EO sterilizers for over a decade now, and I can’t tell you how many times a customer has called me panicking, saying, “My cycle time’s too long, or my microbial reduction isn’t hitting spec,” only for us to trace it back to a wonky gas mix. Let’s break this down straight, no jargon fluff, because this is stuff that actually moves the needle on your sterilization performance. Industrial EO Sterilizer

First, let’s get the basics right: EO sterilization doesn’t work with pure ethylene oxide. Pure EO is super flammable—like, explosive-if-it-heats-up pure. OSHA and EPA guidelines mandate mixing EO with a “carrier gas” to lower that flammability risk. The two most common carriers we use for our sterilizers are hydrofluorocarbons (HFCs, like R134a) and carbon dioxide (CO2), though a few older setups use dichlorodifluoromethane (CFC-12) but that’s phased out for ozone depletion reasons. The mix ratio is the percentage of EO in the total gas volume, and it’s way more critical than most operators realize.
Here’s the science that makes sense, not some textbook gibberish: EO works by alkylating the proteins and DNA of microbes (bacteria, spores, fungi, even viruses) so they can’t replicate. But that reaction relies on EO molecules coming into contact with those microbial cells. If your mix is too low on EO—say, under 10% by volume—there just aren’t enough EO molecules floating around to do the job. The reaction slows way down, your cycle time stretches, and you might not hit that required 6-log microbial reduction (the industry standard for medical devices, meaning 99.9999% of pathogens are dead). We had a medical device startup last year run into this: they used a 8% EO mix, thought their cycle was 4 hours, but their validation failed because only a 4-log reduction was achieved. They cranked that mix to 12% overnight, and boom—their cycle time dropped 25% and they passed their audit.
But wait, flip side: too much EO in the mix is a problem too. We’ve seen customers go over 20% EO, and two things happen. First, the flammability risk creeps up—even with the carrier, higher EO concentrations push closer to the lower explosive limit (LEL). Most modern industrial EO sterilizers have built-in LEL sensors, but why risk it when you can stay well under 50% of the LEL? Second, and less talked about, is post-sterilization aeration time. If you dump too much EO into the chamber, the excess gets trapped in the materials you’re sterilizing (think plastic syringes, silicone catheters, porous packaging). Aeration is the step where you purge the EO residue out before the products go to market—too high an EO mix means you’re aerating for days, tying up your sterilizer and delaying shipment. One of our big clients in the dental supply space had this issue; they were using 22% EO, and their aeration time was 72 hours. We adjusted their ratio to 14%, and aeration dropped to 40 hours, so they could run 20% more batches a week.
Now, it’s not just EO percentage—wait, no, it’s also total gas pressure. The ratio isn’t just volume percentage, it’s partial pressure of EO. That’s a key point I drill into every new customer. For example, a 12% EO mix at 10 psi total chamber pressure means EO partial pressure is 1.2 psi, same as a 12% mix at 15 psi would be 1.8 psi. Higher EO partial pressure means more molecules colliding with microbes, so the reaction is faster. But you can’t just jack up total pressure infinitely—some plastics can’t handle high psi; they warp or leach chemicals. We always adjust ratios to match the materials being sterilized. For heat-sensitive thin films, we use a 10% EO mix at 8 psi to avoid material damage, while for rigid silicone implants that can handle more pressure, we bump to 15% EO at 12 psi for faster cycles.
Another underrated factor: carrier gas type affects ratio performance. CO2 is heavier than HFC, so it displaces air more evenly in porous loads—like wrapped surgical instruments or gauze—so a 12% EO/CO2 mix works better for those. HFC is lighter, so it’s better for non-porous items, like metal surgical tools, where you don’t want heavy gas pooling on the bottom of the chamber. We recommend testing both for a load type, but 9 times out of 10, matching carrier to load cuts cycle time by 15% minimum.
Wait, let’s talk about validation, because that’s what keeps you compliant with FDA, CE, ISO, all those bodies. You can’t just pick a ratio and hope it works; you have to validate that your mix gives you the right log reduction. We’ve had customers use a generic 10% ratio from an old manual, but when we tested it with their specific load, they only got a 3-log reduction. Why? Because their load was tightly wrapped and didn’t let the gas penetrate. So we adjusted the ratio to 13% and bumped the exposure time 10 minutes, and they passed. That’s not a failure of the sterilizer—it’s a failure of not tailoring the ratio to your actual load.
I also want to clear up a myth a lot of folks have: “Higher EO ratio = better sterilization, always.” No way. We once had a customer try 25% EO for a batch of disposable masks, and their residual EO levels were way over the limit (0.5 ppm for Class I medical devices, per FDA). Even after a 5-day aeration, they were at 1.2 ppm. We dialed them back to 11% EO, and aeration only took 36 hours, with residues coming in at 0.3 ppm. That’s the balance, right? You need enough EO to kill all microbes, but not so much that residues pile up or you risk explosions.
Now, how do our sterilizers handle this ratio stuff, anyway? All our industrial EO units have adjustable ratio controls, not fixed mix chambers. That means you can tweak the EO percentage, carrier gas type, pressure, and exposure time to your exact load, not a one-size-fits-all setting. We also have built-in sensors that monitor the ratio in real time during the cycle—if it drops below your set point, it top-ups automatically, so you never have a weak spot in the chamber. That’s a game-changer compared to older sterilizers where the ratio was fixed, leading to inconsistent performance.
I’ve also seen customers cut corners on ratio to save money. EO is more expensive than carrier gas, so some try to use a lower EO mix to lower their gas costs. But let’s do the math: if your cycle fails, you have to reprocess or scrap the entire batch. A batch of surgical instruments that costs $50k to produce, if it fails because your ratio was too low, that’s way more loss than you’d save by using 2% less EO per cycle. We always tell customers: invest in the right ratio, don’t cut corners. It saves you way more in the long run.
Let’s wrap this up with a quick example of a real customer win, because that’s what this is all about. A few months back, a biotech company was using a competitor’s EO sterilizer, and their performance was all over the place—some batches passed, some failed, cycle times varied by 2 hours. They called us because they were struggling to meet their production deadlines. We swapped their old fixed-ratio chamber for our adjustable ratio system, tested their load (porous cell culture trays), landed on a 12% EO/CO2 mix at 10 psi, and adjusted their exposure time to 90 minutes. After validation, their failure rate dropped to zero, cycle time went from 6 hours to 3.5 hours, and they increased their weekly production by 40%. That’s exactly how ratio impacts performance—it’s not a small detail, it’s the core of consistent, efficient sterilization.
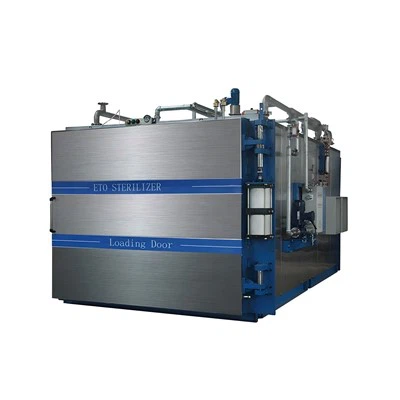
If you’re here because you’re shopping for an industrial EO sterilizer, or you’re having trouble nailing the right gas mix for your loads, I’m your guy. We’ve worked with hundreds of facilities across medical, pharma, and device manufacturing, and we can help you dial in the perfect ratio for your specific products, no generic advice, no fluff. We’ll even do a free load validation test for you to make sure your sterilizer and gas mix are working as they should. Don’t let a wonky gas ratio mess up your sterilization process—reach out to us, and we’ll get you set up for consistent, compliant performance.
Industrial EO Sterilizer References
- ISO 11135:2014, Sterilization of health care products—Ethylene oxide—Requirements for the development, validation, and routine control of a sterilization process for medical devices.
- OSHA Technical Manual (OTM), Section IV: Chapter 4, Ethylene Oxide.
- U.S. Food and Drug Administration (FDA), Guidance for Industry: Ethylene Oxide Sterilization of Medical Devices.
- Rutala, W. A., & Weber, D. J. (2016). Sterilization and Disinfection in Health Care Settings. Clinical Microbiology Reviews.
Hangzhou Riches Engineering Co., Ltd.
Hangzhou Riches Engineering Co., Ltd. is one of the most professional industrial eo sterilizer manufacturers and suppliers in China, specialized in providing high quality custom service and ODM service. We warmly welcome you to buy high-grade industrial eo sterilizer for sale here from our factory.
Address: No. 368, Wenjiao Road, Fuyang District, Hangzhou
E-mail: jason@riches-company.com
WebSite: https://www.eto-sterile.com/
