Hey there, if you’ve ever stood in a hydraulic parts factory watching gear pumps get machined or cylinder bodies get honed, you might’ve thought, “Why does this equipment cost so much?” Trust me, I’ve been there—been on the supplier side for hydraulic industry production gear for over a decade, and let’s cut to the chase: the materials we use to build that equipment aren’t just “metal stuff.” They’re non-negotiable, because hydraulic systems run on pressure, heat, and constant wear that’ll eat flimsy gear alive. Today, I’m breaking down exactly what we (as your go-to hydraulic production equipment supplier) insist on for every machine we ship—no jargon, no fluff, just the real deal. Hydraulic Industry Production Equipment
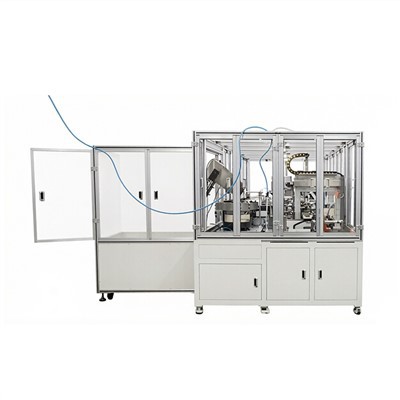
First off, let’s start with the big one: the structural frame of the production equipment. This is the backbone—think of it as the bones holding every spindle, hydraulic actuator, and control unit together. If the frame bends or flexes mid-operation, your machining precision goes out the window. I’ve seen cheap suppliers cut corners here using regular mild steel, which warps faster than a pizza left in a hot car. We use high-grade carbon steel—specifically A36 for most general runs, but we step up to HSLA (high-strength low-alloy) steel for heavy-duty stuff, like equipment that machines 2-inch thick cylinder barrels or runs 24/7 for months. Wait, and we never skip the stress-relieving heat treatment either—no exceptions. That’s the process where we heat the frame to like 1,100°F and let it cool slow to get rid of all the internal stresses from welding. I learned that the hard way early in my career: shipped a batch of frame saws that didn’t get stress-relieved, and half came back with twisted bases after a week of running. Never again.
Next up, the core machining components—things like the spindles, tool holders, and linear guides. These are the parts doing the actual cutting, boring, or shaping of your hydraulic parts, so they need to hold tight tolerances (think ±0.001mm, that’s thinner than a human hair) for years. For spindles? We go with high-speed steel (HSS) for standard jobs, but when we’re talking about precision CNC machines that make hydraulic valves? We use solid carbide. Carbide is way harder than steel—like, diamond-hard level of hardness, and it resists wear so good that a carbide spindle might last 10 years before needing a regrind, vs. HSS which would go in 2. And linear guides? Forget the cheap chrome-plated steel that rusts if you so much as spill a drop of coolant. We use case-hardened chrome vanadium steel. Case-hardening means we only harden the outer 1-2mm of the guide, so it’s tough enough to handle the constant sliding of the machine table, but the inner core stays flexible enough to not crack if something heavy slams into it. I’ve had clients tell me they tried a budget linear guide set from a no-name supplier, and within 3 months, the table was wobbling so bad their valve ports were leaking oil. Ouch.
Wait, can’t skip the hydraulic actuators and pumps that are on the production equipment itself—right, because the machine that makes your hydraulic parts uses hydraulics too. These are the workhorses for clamping parts, moving tables, lifting workpieces, so they need to handle massive pressure, often under continuous load. For actuator cylinders, we don’t use standard cast iron—we use seamless cold-drawn steel tubing. Cold drawing makes the tube’s inner surface super smooth, which cuts down on seal wear and leaks. And the pistons? We go with ductile iron, not gray iron. Gray iron is brittle—if you apply too much pressure, it shatters like a wine glass. Ductile iron has graphite nodules that make it flexible, so it can bend a little under pressure without breaking. Plus, we coat all moving surfaces with hard chrome plating—another non-negotiable. That coating is like a shield against corrosion and friction, so your actuator won’t seize up after a year of running in a dusty factory. I once visited a client who used uncoated actuators in a sawmill-adjacent factory (super dusty, humid), and their actuators were seizing so often they had to replace them every 6 months. Switch to coated, and they’re at 3 years now.
Oh, and the cutting tools—wait, these are materials too, right? Because the tools that machine hydraulic parts (like valve spools, gear pump gears) have to handle abrasive materials. If you’re machining bronze or cast iron (common for hydraulic parts), regular HSS tools will dull in an hour. We use coated carbide tools here—specifically TiAlN (titanium aluminum nitride) coating. That coating can handle temps up to 1,400°F from cutting friction, so the tool doesn’t soften and wear. I tested a batch of uncoated tools once vs. TiAlN-coated: uncoated took 20 minutes to machine a set of gear gears, with a rough finish; coated finished in 5 minutes, and the finish was so smooth they didn’t need secondary grinding. That’s the kind of productivity we’re all after.
Wait, what about all the smaller, “invisible” materials? The seals, fasteners, coolant lines? People sleep on these, but they break everything. For seals on our production equipment’s actuators and hydraulic circuits, we use nitrile butadiene rubber (NBR) for standard temps, but if your factory runs hot (over 180°F), we switch to Viton. I had a client in a desert plant who used NBR seals—they cracked in 2 months from the heat. Switched to Viton, and no leaks since. Fasteners? We never use regular zinc-plated steel bolts. We use alloy steel bolts with hot-dip galvanizing or Cadmium plating. Hot-dip galvanizing is great for outdoor or humid environments, Cadmium for high-heat applications because it resists corrosion way better. Coolant lines? We use reinforced nylon, not rubber. Rubber lines get soft and leak under high-pressure coolant, while reinforced nylon can handle up to 150 PSI without bulging, and it’s resistant to most cutting fluids.
And let’s not forget about the control system components—wait, these are materials too, right? The circuit boards, sensors, enclosures. For enclosures, we use powder-coated aluminum or stainless steel, not plain steel that rusts. Sensors? We use proximity sensors with stainless steel housing, not plastic, because plastic cracks from oil and vibration. I once had a client install plastic proximity sensors in a shop with a lot of oil mist, and the sensors stopped working in a month because the oil ate through the plastic housing. Stainless steel housing fixes that.
Now, why do I (as a hydraulic production equipment supplier) care so much about all this? Because I’ve seen what happens when you cut corners on materials. A cheap machine might save you 20% upfront, but it’ll break down every 3 months, costing you thousands in downtime and repairs. Our equipment might cost a little more, but it runs 24/7, holds tight tolerances, and lasts a decade or more. That’s the real value here.
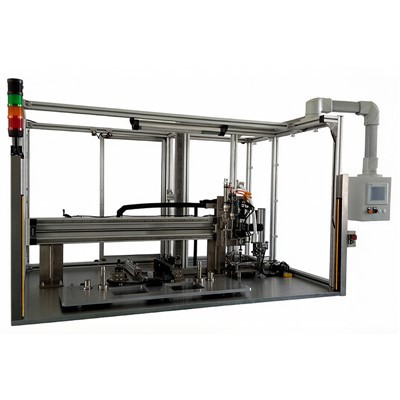
If you’re currently shopping for hydraulic production equipment, and you’re tired of machines that break, are off-spec, or leak oil, hit me up. We can walk through your specific needs—whether you’re making small valve parts or big hydraulic cylinders—and build a machine that uses the right materials for your job. No generic gear, no shortcuts, just equipment that works as hard as you do.
Packaging Industry Production Equipment References:
- Hydraulic Machinery Design and Materials Selection, Society of Manufacturing Engineers, 2021.
- Tribology for Manufacturing Equipment, International Journal of Machine Tools and Manufacture, Vol. 68, 2013, pp. 45-52.
- Sealing Materials for Hydraulic Systems, Fluid Power Technology Association, 2020.
- High-Speed Machining Tool Materials, Journal of Manufacturing Processes, Vol. 22, 2016, pp. 112-118.
Shanghai Zenyan Automation Engineering Co., Ltd.
As one of the leading hydraulic industry production equipment manufacturers in China, we warmly welcome you to buy advanced hydraulic industry production equipment made in China here from our factory. All customized machines are with high quality and low price. Contact us for quotation.
Address: 3rd Floor, Building A, No.5629 Beisong Road, Chedun Town, Songjiang District, Shanghai, China
E-mail: zenyan_sh@163.com
WebSite: https://www.zenyanauto.com/
